This guide explains how to evaluate the 750816 item for procurement decisions, with a focus on supplier verification, specification matching, and procurement readiness. Objectively, “750816” is treated as an internal or catalog identifier used in sourcing workflows. In practice, buyers compare equivalent specs across vendors, review lead times and documentation, and confirm quality controls before purchase.
When sourcing an item identified as 750816, the fastest path to a reliable procurement outcome is to treat it as a specification-driven purchasing task rather than a name-based search. In practical supplier workflows, “750816” functions as a reference code that must be matched with the correct material, tolerance, finish, and documentation. If you approach it with a structured verification routine—supplier qualification, item equivalence checks, and risk-based inspection planning—you reduce costly rework and returns.
From an industry standpoint, buyers generally succeed when they can clearly answer three questions: (1) What exact configuration does 750816 represent? (2) Which supplier can reliably deliver it with acceptable consistency? (3) What evidence supports quality claims (inspection reports, traceability, testing results, and packaging/handling controls)?
In other words, “finding 750816” is only step one. The procurement win comes from ensuring that the delivered part is actually the part you designed around, certified around, or qualified around—at the correct revision level, with the documentation and traceability that your downstream process expects.
This matters because part numbers (including 750816) can remain constant while internal manufacturing can evolve: supplier processes change, sub-tier materials shift, tolerances are tightened or inadvertently drifted, coatings get updated, or documentation revisions lag behind physical changes. Treating the part number as the entire truth source invites mismatch. Treating it as a key to the correct specification—and validating that specification at receiving—creates dependable outcomes.
Accordingly, the first confirmations you should make are: (a) the governing technical document for 750816 (drawing/datasheet with revision), (b) the supplier’s ability to meet that exact configuration consistently, and (c) the quality evidence you will receive and verify at shipment/receiving. Once those three are settled, pricing, lead time, and logistics can be optimized with far less uncertainty.
750816 is typically used as a catalog number, part code, or internal SKU within an organization or supply chain. Depending on the industry, such codes may correspond to a specific product configuration (for example, a particular size, material grade, coating, or assembly variant). Because supplier catalogs sometimes use similar numbering conventions, identical-looking codes can occasionally be accompanied by different revision histories or manufacturing specifications.
For that reason, the code itself should not be the only determinant. Buyers commonly cross-check the code against a specification sheet, drawings, or testable attributes (dimensions, surface condition, performance characteristics, packaging requirements, and compliance documentation where applicable). This is especially important when purchasing from different regions and manufacturers, where terminology and catalog structure may vary.
It’s also common to find that “750816” appears in multiple contexts: as a standalone component, as part of a kit, or as an assembly that includes multiple materials/components. In those cases, the supplier’s item listing may compress details that your receiving department will still need to validate. You may receive a package labeled “750816,” but the contents could represent a variant (e.g., different surface treatment) unless your PO and acceptance criteria explicitly guard against that.
Another practical background point: some organizations use numeric identifiers internally that do not fully map to public catalogs. For example, “750816” could be a customer-specific code used by your engineering team, but the supplier might source the underlying item from a standard product with a different catalog number. The supplier can still deliver correctly, but you must require a clear “mapping” statement in documentation: the delivered item must identify which internal or sub-supplier part number it corresponds to, and it must still match your engineering specification.
Finally, revisions matter. Even if the part number does not change, a drawing revision may alter material specification, manufacturing route, plating thickness, heat treatment parameters, or allowable cosmetic defects. If revision control is not enforced, teams may believe they ordered 750816 “as usual,” when in reality the “as usual” is no longer the same configuration.
In professional sourcing, supplier credibility is built through documentation and process evidence, not promotional language. For an item like 750816, consider the following verification steps as part of your standard vendor onboarding and ongoing supplier management.
Supplier selection has two dimensions: (1) whether they can build the part to your specification, and (2) whether they can do it repeatedly with stable quality under normal operational fluctuations (demand spikes, raw material variability, workforce changes, machine maintenance cycles, and logistics disruptions).
When you treat supplier selection as an evidence-based task, you can avoid a common failure mode: choosing a supplier who can pass once during qualification but cannot sustain the same performance in later lots. That failure is particularly risky when the part number is embedded in production planning assumptions and your process depends on consistent dimensional/functional performance.
To make these requests operationally effective, ask for them in a “PO-ready” form. For example, request a document list that states the exact document names and issue/ revision levels your organization will receive with each shipment (or at least with each lot). Avoid receiving documents that are generic templates not tied to your part number or not tied to the relevant drawing revision.
Also consider requesting a “manufacturing route summary” (what key steps are performed), especially if the quality of 750816 is sensitive to the manufacturing route. For example, in metal parts, the route can determine residual stress and surface hardness; in electronics, it can influence solderability, dielectric performance, or contamination levels. Even if you don’t fully audit the route, a clear description helps you design the right inspection and testing approach.
Even when the part code matches, inconsistency can arise from manufacturing changes, supplier capacity constraints, or changing sub-tier inputs. Ask about current production status, typical lead times under normal conditions, and how the supplier handles demand variability. If the supplier claims a particular turnaround, the buyer should request how that timeline is managed operationally—such as material availability, production scheduling, and dispatch/transport procedures.
It’s also valuable to clarify what lead time you should plan for: quoted “order-to-ship” time, or “order-to-receiving” time after transport. Procurement teams often see schedule surprises because suppliers quote manufacturing time but do not include transit time, customs clearance (if applicable), consolidation delays, or warehouse processing time.
Consistency questions to ask include:
These questions help you assess not only whether supplier A “can deliver” but whether supplier A can deliver with a predictable quality profile that reduces your internal burden.
Because the prompt you provided does not include explicit numeric price figures, the very objective approach is to describe how to interpret price for 750816 rather than inventing numbers. In real procurement practice, a “unit price” can be misleading unless you also model shipping, packaging, inspection, and potential replacement costs due to mismatch risk.
Industry buyers usually evaluate total procurement cost using a framework like this:
Where possible, request quotes that reflect the same scope: same packaging, same documentation set, same acceptance criteria, and the same revision of the product. This ensures the comparison is apples-to-apples.
It can also be helpful to separate quote components to avoid hidden cost tradeoffs. For example, a supplier may quote a lower unit price by excluding certain documentation, shipping insurance, or test certificates. If your downstream process requires those documents, the “savings” may vanish when your team pays for expedited shipping, additional inspection, or re-certification.
Similarly, when the part is controlled by revision level, any quote that does not explicitly state the revision level (or uses vague language like “latest revision”) should be treated as incomplete. If you need a specific revision for qualification reasons, the price comparison must be based on that exact revision.
Another procurement nuance: if 750816 is time-critical, ask about expediting capability and cost. If you repeatedly receive schedule pressure, negotiate service-level expectations and pricing for emergency production. That can reduce the frequency of expensive last-minute actions.
Finally, if your organization tracks cost of poor quality (COPQ), include the practical quality costs in your evaluation: first-pass yield at receiving, the cost of quarantining nonconforming stock, and the cost of rework if parts must be corrected. A slightly higher unit price can be cheaper in the long run if it reduces mismatch risk and inspection burden.
For a procurement decision involving 750816, “supplier details” should be more than a vendor name. An industry-ready supplier profile usually includes:
If you are comparing multiple suppliers, focus on evidence of repeatability. A quote that is only credible “on paper” but lacks consistent documentation is a procurement risk.
To deepen “good enough” supplier data, also request the ability to provide a consistent packaging method. For parts that are sensitive to handling (corrosion-prone coatings, delicate finishes, or components that can deform), packaging becomes part of quality. If a supplier ships without protective measures, quality can degrade during transit even when the part is manufactured correctly.
Another key supplier detail is the clarity of their corrective action process. When nonconformance occurs, you need to know whether they can perform root cause analysis, provide containment details, and prevent recurrence. Ask for examples of how they handled a similar NCR (if sharing is possible) or at least describe their typical corrective action lifecycle: containment, root cause, corrective action, verification, and documentation release.
Procurement mistakes often begin at the translation layer: one party believes 750816 refers to a configuration that the other party manufactures differently. This is why an expert sourcing process includes a structured specification matching approach. The core idea is simple: confirm that the supplier understands your target requirements and that you can validate them through documentation and inspection.
Specification matching is not merely administrative. It is the technical “contract” between your design intent and the supplier’s manufacturing outputs. A buyer who ensures specification matching can reduce ambiguity and also reduce internal conflicts later (engineering vs. quality vs. purchasing vs. receiving) because everyone uses the same source-of-truth.
To confirm 750816 is truly the item you intend to procure, you can compile a checklist of testable and documentary elements such as:
To make the checklist more practical, convert it into two layers: a “documentation layer” and a “physical verification layer.” The documentation layer confirms that the supplier claims align with your engineering intent. The physical verification layer confirms that the delivered item actually meets those claims.
For example, if 750816 requires a specific coating thickness, the documentation layer might request a certificate or test report that indicates the thickness measurement method. The physical verification layer might include dimensional or coating verification at receiving using your method (or supplier-provided measurement results, if validated). This reduces the risk that you only have paperwork but not measurable reality.
When the part is critical or the risk of mismatch is high, staged purchasing reduces exposure. A typical approach is to order a limited quantity for qualification testing, verify acceptance against your criteria, and then scale volumes if the results remain consistent. Even if a supplier has strong credentials, qualification helps confirm that the delivered lot matches your specific use case.
Staged buying is also useful when documentation is available but not fully trusted yet. For example, a supplier might provide a datasheet tied to 750816 but may not have a strong track record with your specific revision. By testing a small lot, you validate both the technical and traceability aspects before committing to production volumes.
In some cases, qualification should include not only “does it meet specs” but “does it meet your manufacturing needs.” For instance, if 750816 is used in assembly, test whether the part’s physical characteristics allow proper installation without additional machining or rework. If it is used in a device, test whether it meets functional performance requirements under realistic operating conditions.
Be mindful that staged purchases should also validate logistics. A staged buy can reveal whether packaging prevents damage, whether labeling matches receiving systems, and whether traceability documentation is correctly included in the shipment.
After confirming the specification and supplier credibility, operational readiness is what turns a vendor agreement into predictable delivery. While exact procedures vary by organization, professional procurement teams align the order with clear acceptance rules and communication channels.
Operational readiness reduces friction across departments and minimizes delays when something goes wrong. For example, if a shipment arrives late or with incomplete documentation, the receiving team should have clear instructions on how to handle it—who to contact, what to quarantine, and what documentation constitutes acceptable compliance.
Operational readiness also ensures that “750816” is not treated differently by each internal team. Purchasing, quality, logistics, and engineering should all reference the same revision and acceptance criteria.
To extend operational readiness, consider implementing a “receiving checklist” that mirrors your PO requirements. This checklist should include: verifying revision level on packing slip/labels, verifying packaging condition, verifying presence of required documentation (e.g., certificate of conformance, test reports), and performing physical checks as required. When a receiving checklist is used consistently, you avoid the time-consuming scramble that happens when disputes arise.
Also ensure that your traceability system is compatible with supplier labeling. If your warehouse expects a certain format or set of fields, confirm that supplier labels include the necessary information (lot number, date code, revision, and part number). Otherwise, you may receive a correct physical item but cannot properly track it through your system.
Quality and supply risk are typically managed through a combination of vendor governance and receiving controls. Reliable suppliers mitigate risk through stable manufacturing processes and documented quality systems, while buyers mitigate risk through specification control and inspection planning.
Important context: many industries track supplier nonconformance using internal KPIs (e.g., defect rates, return rates, and corrective action cycle times). However, since your prompt does not specify a sector (automotive, electronics, healthcare, industrial components, etc.), introducing numerical “industry averages” could be misleading. The very responsible approach is to use a process you control—qualify the specific supplier and lot for 750816, define acceptance criteria, and measure outcomes in your own environment.
Risk management should also be proportional. Over-inspection increases cost and can slow down production schedules; under-inspection increases risk of downstream failures and costly returns. The correct balance depends on criticality, historical performance, and how hard it is to verify the part (some characteristics are difficult to test quickly at receiving).
A practical risk framework often includes:
Once you establish this, your inspection plan can be aligned to risk—e.g., tighter sampling early in a supplier relationship, expanded documentation requirements for first lots, or additional testing for parts with performance-based requirements.
Risk management also includes regulatory or compliance considerations where applicable. If 750816 is used in a regulated product (medical, aerospace, defense, food-contact, or safety-critical equipment), you may need compliance evidence beyond standard dimensional checks. In those cases, risk management must ensure that the documentation you request matches regulatory expectations and that suppliers can consistently generate it.
The following table summarizes common approaches to 750816 procurement. It is a comparison framework, not a claim about a specific vendor or location.
| Procurement approach | Top for | Key requirements / conditions | Primary verification evidence |
|---|---|---|---|
| Full documentation match | High criticality parts where revisions matter | Receive datasheet/drawing tied to 750816 revision; confirm materials and tolerances | Specification sheet, revision history, test reports (as applicable) |
| Staged qualification purchase | New supplier onboarding or first-time usage | Order limited quantity; define acceptance tests before scaling | Incoming inspection results, qualification test outcomes |
| Supplier quality governance | Recurring orders across multiple lots | Documented corrective action process; traceability expectations in PO | Quality system evidence, lot traceability records, NCR handling documentation |
| Receiving inspection optimization | Balancing cost and quality assurance | Sampling plan aligned to risk; documented pass/fail rules | Inspection logs, statistical sampling records (where used) |
To further strengthen the step-by-step flow, you can add two “operational guardrails” that often prevent downstream disputes: (1) enforce a documented “change control rule” (what happens if the supplier proposes a change), and (2) enforce a “documentation completeness rule” (what happens if the shipment lacks required certificates or revision identifiers).
In practice, many procurement delays occur not because the part is unavailable, but because the shipment arrives without the documentation package. When you define documentation completeness requirements upfront, receiving can accept/reject based on clear criteria rather than subjective judgment.
For consistent outcomes with 750816, include the following conditions in your procurement process:
Depending on the part’s use case, you may also need special requirements. For instance, some parts require environmental controls (humidity-sensitive packaging), special handling (anti-static for electronics, torque limits for fasteners, or protective wrapping for coated surfaces), or specific shelf-life declarations. If 750816 is sensitive to such factors, your PO should reflect them.
It can also be beneficial to specify what “accepted” means for appearance. A supplier may meet dimensional criteria but have cosmetic defects (scratches, nicks, stain marks) that can violate your acceptance standards or impact downstream assembly. If cosmetic tolerances are defined in your engineering documentation, reflect them explicitly in your acceptance criteria.
Another practical addition is to include a “rejection and return procedure” in your workflow. Buyers often discover late that they need to quarantine parts but don’t have a clear plan for how to handle returns, replacement shipments, and costs. A well-defined procedure reduces delays and negotiation friction when quality issues occur.
A: In very sourcing contexts, 750816 is a part code, SKU, or catalog identifier. It should be verified against the associated specification, drawing, and revision details rather than treated as a standalone description.
A: Request the same supporting documentation for 750816 (datasheet/drawing, materials/process details, and revision level). Then validate testable attributes through receiving inspection and, if required, staged qualification.
A: Ask for a quote that clearly states unit cost under the same scope: revision level, documentation set, packaging requirements, lead-time conditions, shipping terms, and any inspection/testing deliverables that affect total procurement cost.
A: Professional procurement typically treats supplier claims as a starting point. Quality assurance should be supported by documentation and verified through receiving inspection and qualification testing aligned to your acceptance criteria.
A: Initiate an NCR (nonconformance report), quarantine affected stock, document discrepancies against the acceptance criteria, and require corrective action from the supplier. Also assess whether the issue is limited to a lot or indicates a broader process gap.
A: Not always. It is very valuable for first-time supplier relationships, high criticality components, or when specifications/revisions are frequently changing. For established suppliers with strong performance, you may rely on routine receiving inspection with risk-based sampling.
A: Treat revision mismatch as a nonconformance unless your engineering group explicitly approves equivalence. Require the supplier to confirm the revision on the packing slip and documentation package, and compare it against your governing drawing revision. If you receive a different revision, quarantine the lot and investigate what changed (material/process/limits) and whether it is compatible with your application.
A: The strongest evidence is a traceability record that ties lot/batch identification to manufacturing steps and inspection results, typically supported by lot-specific certificates and labels that survive the packaging chain. In practice, you want labels on the packaging and documents that include matching lot IDs, production dates (or date codes), revision level, and part identification that aligns with your PO.
A: Sometimes, but it depends on confidence. If your supplier has demonstrated consistent performance and your acceptance criteria are measurement-method-aligned, you may reduce receiving inspection. However, you should still perform at least verification sampling or confirm critical attributes in a way that matches your risk assessment. If your supplier’s reported tests use different measurement methods, you may need to validate those methods or re-measure critical dimensions.
A: “Drop-in” claims should be treated as an equivalence assertion, not proof. You should request documentation demonstrating compliance with the same revision and acceptance criteria. If the part is critical, validate with staged testing before scaling. “Drop-in” can be true in a functional sense but still fail in documentation requirements, labeling needs, or specific tolerances that matter in your assembly.
Sourcing 750816 successfully comes down to disciplined specification control and evidence-based supplier verification. Instead of focusing only on a code or a unit price, professional buyers define what “correct” means, validate it through documentation and inspection, and then structure orders to minimize ambiguity. Over time, this approach improves consistency, strengthens supplier accountability, and reduces avoidable cost drivers such as rework, returns, and schedule disruption.
If you share the industry context (e.g., electronics component, industrial hardware, automotive part) and the specific documents you already have for 750816, I can help you refine the equivalence checklist and acceptance criteria in a more targeted way.
Ultimately, the reason this approach works is that it converts uncertainty into verifiable inputs: the correct revision becomes explicit, the supplier capability becomes measurable through inspection and evidence, and the procurement risk becomes manageable through staged qualification and risk-based receiving. With that foundation, the code 750816 becomes what it was meant to be—a reliable identifier—rather than a misleading substitute for engineering truth.
A Guide to Cost-Efficient Small Electric Cars for Seniors
Mastering Debt Consolidation: Boost Your Credit Score and Manage Interest Rates
Your Guide to Loans, Credit Checks, and Interest Rates
Affordable Independent Living: Finding the Right Senior Housing
Guide to Senior Living Apartments: Affordable and Comfortable Environments
Leasing a Car: Expert Tips for Your Next Vehicle
Maintaining Oral Health After Tooth Loss with Dental Implants
Maintaining Oral Health with Dental Implants for the Elderly
AntoniaRafaela Buyer Guide for Trusted Supply Decisions
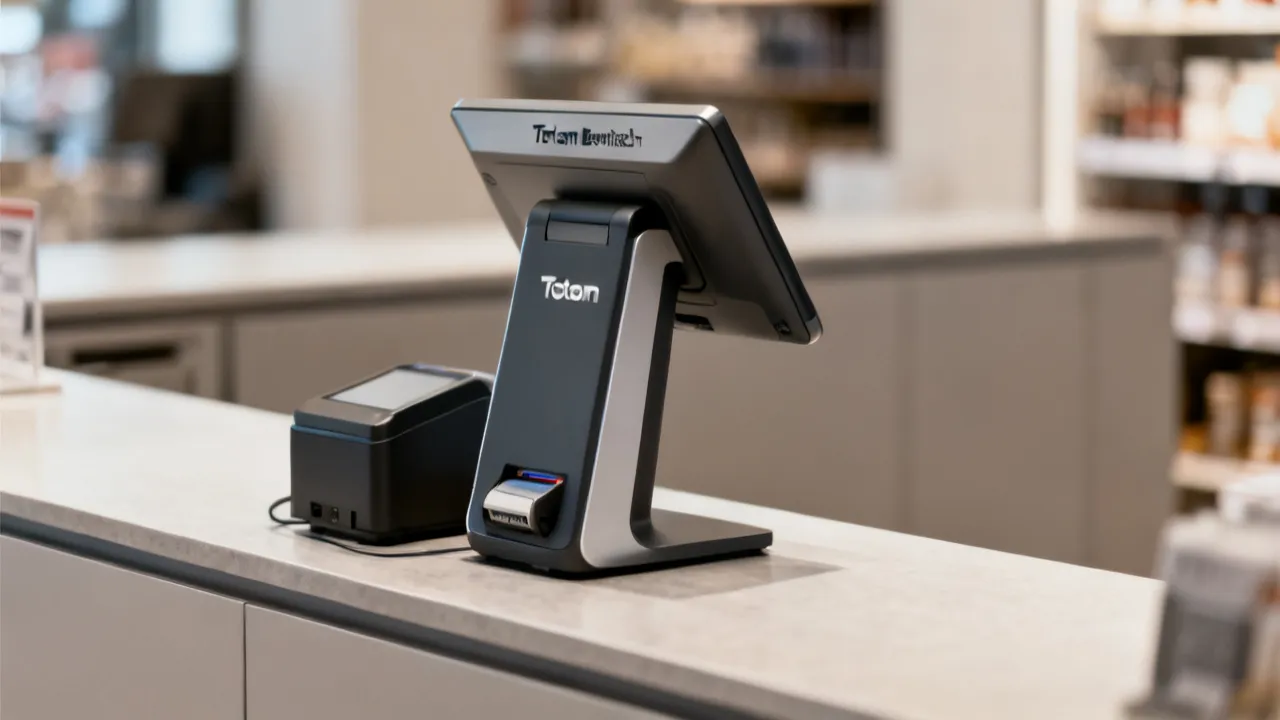
Totem Bematech: Practical Guide for Smarter Retail Operations
Totem Bematech is a retail signage and customer-facing device that helps stores present information, guide service flow, and improve in-counter experience. This guide explains what Totem Bematech typically includes and how it fits into POS and service environments. It also outlines buying considerations, compatibility checkpoints, and practical implementation steps based on common retail IT practices.
Professional Guide to 750816 Product Sourcing
This guide explains how to evaluate the 750816 item for procurement decisions, with a focus on supplier verification, specification matching, and procurement readiness. Objectively, “750816” is treated as an internal or catalog identifier used in sourcing workflows. In practice, buyers compare equivalent specs across vendors, review lead times and documentation, and confirm quality controls before purchase.